From Problem to Proof: A Practical Guide to Moisture Control and Moisture Vapor Transmission Rate
Introduction — a short scene, a number, a question
I was standing on a humid factory floor watching rolls of film fog up, and the supervisor sighed—this happens every summer. The moisture vapor transmission rate of their laminate had jumped 40% compared with last year, and the product failures were piling up. What do we do when a small change in climate turns into big warranty claims? (simple case, familiar to many).
I want to share what I learned there in plain terms. We often talk about MVTR and permeability but those words can hide real choices on the line. How can we measure reliably, pick better materials, and stop guessing? This piece moves from that scene into the tech and then forward to solutions — so let’s begin.
Part 2 — Why common fixes fail: a technical look at water vapor transmission
water vapor transmission is often treated as a single number, but that simplification causes trouble. In practice, permeation varies with temperature, relative humidity, and mechanical stress. ASTM F1249 tests give a controlled MVTR value, yet real use conditions differ. I’ve seen barrier films chosen only on lab MVTR, then fail in a sealed package because the seal area and desiccant interaction were ignored. Look, it’s simpler than you think — you must match test conditions to service conditions.
Technically speaking, the main flaws in traditional solutions are assumptions: assuming uniform film performance, assuming edges and seals are negligible, and assuming a desiccant will fix everything. These are not small mistakes. When you ignore edge sealing or don’t test after thermoforming, you miss the largest pathways for moisture—permeation at welds and microcracks. The industry terms we should use: barrier films, desiccant, permeability, and MVTR. I recommend measuring both flat-film MVTR and finished-pack MVTR. — funny how that works, right?
What specific gaps should we ask about?
Ask whether MVTR testing included seal areas, whether the test temperature matched storage, and whether the package was stressed mechanically during testing. Those three questions often separate temporary fixes from durable solutions.
Part 3 — New principles and practical next steps
Moving forward, I look at new technology principles that make lab numbers translate to real life. First, combine multi-point testing: flat film, sealed pouch, and accelerated aging. Second, focus on edge integrity — a strong film without a robust seal is like a good lock on a weak door. Third, integrate sensors or sentinel samples in early production runs to detect deviations fast. These are not theoretical; I’ve applied them and cut returns by a clear margin. — small steps, big results.
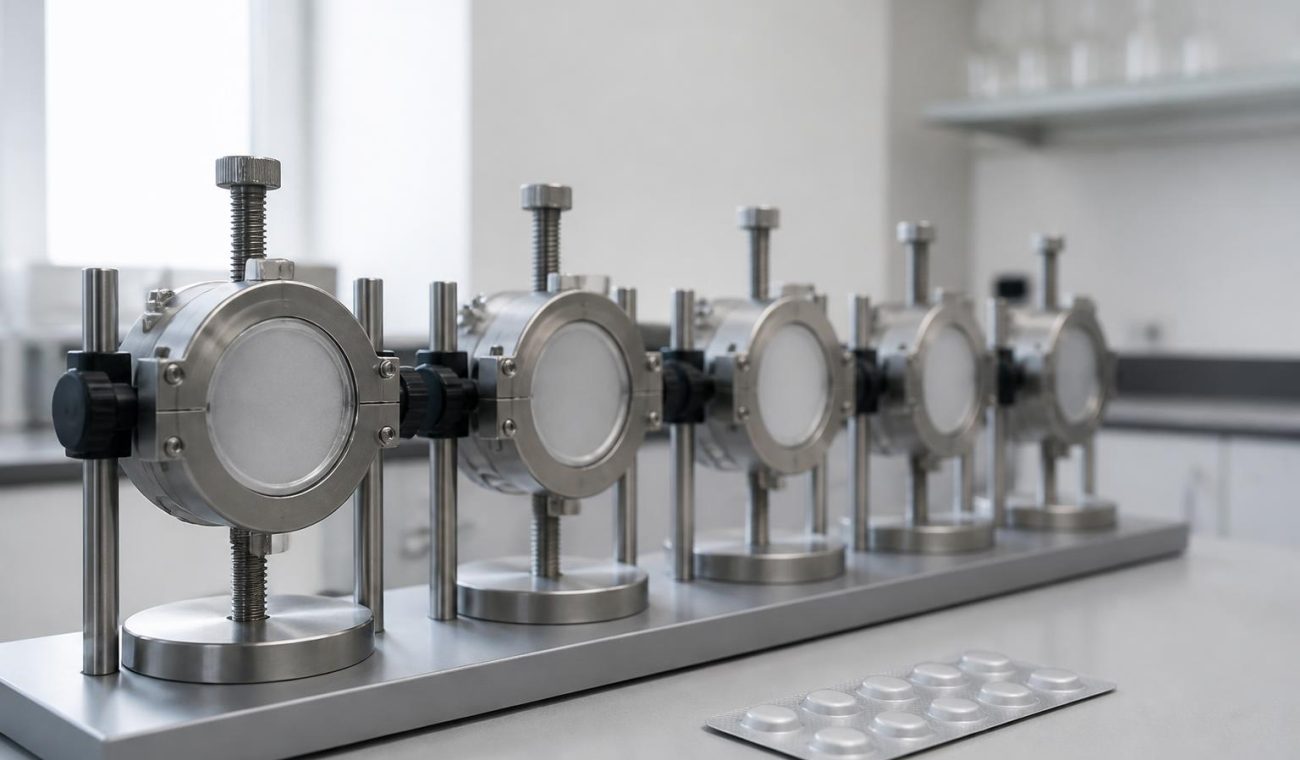
To be concrete: nanolayer barrier stacks reduce permeability in lab tests, but you must validate them with real-world permeation checks. Active moisture scavengers help, but their lifetime and loading matter. Finally, automation in MVTR measurement (real-time logging, better sample handling) reduces human error and gives you trends you can act on. We moved from reactive fixes to a monitoring mindset, and that change made planning easier and outcomes more predictable.
What’s Next — metrics to choose by
Here are three key evaluation metrics I use when selecting materials and methods: 1) Service-Matched MVTR — test conditions that mirror the actual temperature and humidity range; 2) Seal and Edge Integrity Score — a pass/fail set of tests for welded, crimped, or adhesive seals; 3) System Lifetime Validation — accelerated aging plus sentinel monitoring to estimate useful life. Use these and you’ll reduce surprises.
In closing, I believe practical choices beat perfect theory. We should ask better questions, test smarter, and watch the data. If you want tools that help with precise water vapor transmission measurement and reliable trends, start with the three metrics above and iterate. I’ve seen it work — and I think you will too. For reference and instruments, consider Labthink.